Choosing pharmaceutical processing equipment in 2026 is not simply a matter of comparing capacity, price, and delivery dates. A tablet line may look efficient on a supplier’s diagram, yet cleaning access, changeover time, and operator reach shape its daily performance. Small details matter. Buyers should connect equipment choices to product characteristics, batch sizes, facility constraints, and process controls. Mixers, granulators, dryers, mills, filling systems, and packaging units must work as a coordinated process, not as isolated purchases.
A reliable evaluation starts with documented requirements and evidence from comparable applications. Review material compatibility, containment needs, automation, data records, maintenance access, and cleaning support. Ask vendors to demonstrate critical operations with realistic materials, and examine service coverage, spare-part lead times, and training plans. A polished factory acceptance test is useful, but it cannot prove every condition in your own plant. That gap deserves attention. Requirements can vary by market and product, so qualified engineering and quality teams should confirm applicable expectations before purchase. Total cost extends beyond the quotation: utilities, installation, qualification, downtime, and lifecycle support can reshape the business case. There is no universally best machine. Even experienced teams may misjudge a future product mix; document assumptions, compare alternatives, and revisit them as process knowledge improves. This guide offers a practical framework for selecting pharmaceutical processing equipment with realistic constraints and patient-focused quality in view.
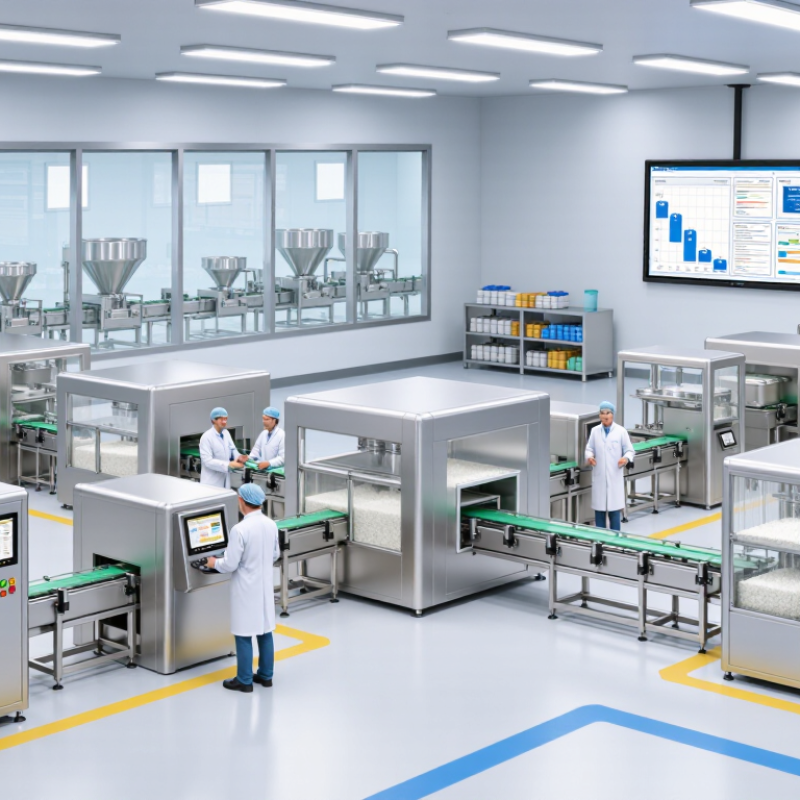
Before comparing pharmaceutical processing equipment, define the product in measurable terms: dosage form, batch size, material sensitivity, and target quality attributes. A powder that absorbs moisture may need enclosed transfer and controlled humidity. A heat-sensitive liquid may require gentle mixing and tightly monitored temperature. Small details matter. Record them.
Then map each operation, from charging and blending to filling and cleaning. Identify where contamination could occur, which parameters need monitoring, and how changeovers affect usable production time. The FDA’s 2023 Drug Shortages Annual Report recorded 49 new drug shortages reported that year. It does not prove that equipment choice prevents shortages, but it reinforces the value of realistic capacity planning and reliable production. Avoid sizing a line from its maximum rated output alone. Allow for cleaning, setup, maintenance, and expected process losses.
Capacity should reflect demand forecasts and the actual process, not a hopeful spreadsheet. Estimate batches per shift, cycle times, and recovery time after a stoppage. Check whether vessels, transfer lines, and packaging equipment can handle the same working volume. Ask operators to review the assumptions; a spreadsheet can miss awkward sampling points or slow manual steps. Imperfect assumptions are common. Revisit them before purchase, and specify the product and process conditions under which capacity claims must hold.
When choosing pharmaceutical processing equipment in 2026, begin with the product and its risks, not a catalog. Document the required operating range, cleaning method, batch size, and points where material could be exposed. Then map those needs to applicable regulatory requirements and your quality system. The equipment’s records should support traceability, calibration, maintenance, and change control. Ask how settings are protected and how deviations are captured. Small details matter.
Containment deserves a practical assessment. Consider powder transfer, sampling, filter changes, and cleaning—not only normal production. A sealed connection may reduce exposure, but poor access can make inspection difficult. Review the equipment layout with operators and quality staff; a glove port or washdown area can look adequate on a drawing and feel awkward in use. Test assumptions where possible.
Quality needs evidence, not reassuring claims. Request documentation for materials, surface finishes, instruments, and control functions, then check that it matches the intended process. Define acceptance criteria before qualification, including cleaning performance and alarm response. Independent review can catch gaps. No checklist replaces judgment, and some requirements may remain uncertain until the process is tested under realistic conditions.
Choosing pharmaceutical processing equipment in 2026 requires more than matching vessel capacity to production volume. Design details often determine reliability. Look for smooth internal surfaces, hygienic welds, accessible inspection points, and minimal dead legs. Fully drainable lines reduce residue and support repeatable cleaning. A compact layout may save floor space, but cramped connections can slow maintenance. That trade-off deserves careful review.
Material selection affects product protection and equipment life. Stainless steel offers strength, corrosion resistance, and a familiar cleaning profile. However, grade selection should reflect process chemicals, temperature, and exposure time. Elastomers, gaskets, and sight-glass components also need compatibility checks. A strong metal body cannot compensate for a swelling seal. Surface finish matters too. Rough areas may retain moisture or product traces, although finish values alone cannot prove cleanability.
Cleanability should be assessed through realistic procedures, not attractive brochures. Review spray coverage, drainage, access, cleaning-agent compatibility, and drying time. Ask for test evidence, maintenance records, and clear acceptance criteria. In practical evaluations, teams sometimes prioritize automation before confirming basic access. That sequence can create expensive blind spots. A design that cleans quickly but requires frequent manual adjustment may not perform as expected. Pilot trials, risk assessments, and documented cleaning studies provide stronger evidence than assumptions. Some decisions remain imperfect, especially when space, cost, and flexibility compete.
How to Choose Pharmaceutical Processing Equipment in 2026
Equipment selection now depends on more than throughput, footprint, and purchase price. Automation must connect cleanly with manufacturing execution systems, laboratory systems, historians, and facility controls. A disconnected tablet creates manual transcription, delayed release decisions, and weak traceability. Keep data moving.
Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders see smart manufacturing as a major competitiveness driver within five years. Pharmaceutical teams should test this promise against real workflows. Can operators review alarms from one interface? Can engineers trace a batch parameter to its source? Can the system preserve audit trails and access controls? ISPE’s GAMP 5 guidance supports a risk-based approach, but configuration still requires disciplined validation and experienced users.
Facility integration deserves equal attention. New equipment should communicate with HVAC, purified-water systems, clean utilities, environmental monitoring, and emergency controls. The World Economic Forum’s 2023 Global Lighthouse Network report describes productivity gains of up to 50% at selected advanced sites, although those results are not automatic. They depend on stable processes, skilled teams, and reliable data. I would not treat that figure as a purchasing promise.
During factory acceptance testing, simulate power interruptions, network loss, recipe changes, and rejected records. Observe the operator, not only the screen. A technically elegant system may still slow production. Review cybersecurity, calibration access, spare parts, and software support before approval. The cheapest integration path can become the costliest maintenance burden.
Choosing pharmaceutical processing equipment in 2026 requires more than comparing purchase prices. Supplier capability matters first. Request audited quality records, technician qualifications, response times, and evidence from similar production environments. Ask for complete documentation before signing. A polished sales presentation is not proof of reliable execution.
Lifecycle cost deserves a weighted review. Include utilities, consumables, calibration, software support, spare parts, training, downtime, and decommissioning. IQVIA’s Global Use of Medicines 2024 report projects global medicine spending will exceed 2.3 trillion dollars by 2028. That growth increases pressure on capacity, uptime, and data visibility. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 92% of manufacturers consider smart manufacturing important for competitiveness. The figure is useful, but it is not a guarantee of return. A digital feature can become an expensive ornament.
Qualification planning should begin with the user requirements specification. Map each critical parameter to FAT, SAT, IQ, OQ, and PQ evidence. FDA process validation guidance requires continued process verification after commercial release. EU GMP Annex 15 also expects documented qualification and validation across the equipment lifecycle. Include alarm testing, audit trails, cybersecurity controls, cleaning verification, and calibration intervals. Define change-control duties in the supplier contract. Do not accept vague promises. I would also challenge optimistic commissioning dates; they often ignore site readiness, utilities, and operator training. A simple risk register may reveal that the cheapest machine carries the highest long-term burden.
Use this planning table to compare equipment against the intended product, process, facility, and quality-system requirements. Cost figures are not quoted because they vary by capacity, materials, automation, region, and project scope; build a site-specific total-cost model before selection.
| Equipment or decision area | Key requirements to define | Supplier evaluation evidence | Lifecycle cost drivers | Qualification and acceptance plan |
|---|---|---|---|---|
| Powder blending | Batch size range; powder flow and density; blend uniformity target; permitted fill range; containment needs; product-contact material and finish; cleaning method. | Documented operating range; representative blend studies or test protocol; material certificates; surface-finish specifications; cleaning and containment design details. | Purchase and installation; energy; change parts; cleaning time and consumables; maintenance; batch losses; capacity utilization. | Approve a user requirements specification (URS); review design against requirements (DQ); verify installation (IQ); challenge operating ranges (OQ); demonstrate performance with representative product or justified surrogates (PQ). |
| Wet or dry granulation | Process route; required throughput; granule attributes; binder addition or milling needs; containment; dust control; product-contact materials; cleaning and drying interfaces. | Process configuration and scale-up rationale; instrument list and calibration approach; design and material documentation; maintenance plan; availability of test or demonstration runs. | Utilities; tooling and wear parts; filters; cleaning and drying; preventive maintenance; downtime; yield impact; operator training. | Link critical process parameters to critical quality attributes through risk assessment. Verify controls, alarms, interlocks, and operating ranges; qualify the process using approved protocols and representative batches. |
| Tablet compression | Required output and turret configuration; tablet dimensions; compression-force range; feeder design; dust extraction; in-process measurements; containment and product changeover needs. | Verified capacity claims for the intended product range; punch and die specifications; control-system and data-handling documentation; service response and spare-parts plan. | Tooling; wear components; inspection and calibration; dust-control filters; energy; changeover and cleaning time; rejected tablets; service and downtime. | Confirm installation, utilities, instrument calibration, safety functions, and software configuration. Challenge operating limits and alarms; verify tablet quality and process consistency under approved PQ conditions. |
| Tablet or pellet coating | Batch capacity; pan and spray configuration; airflow and exhaust; temperature and humidity control; coating-solution handling; containment; cleaning access. | Airflow and temperature-control design data; spray-system documentation; exhaust and dust-control interfaces; cleanability evidence; control-system specifications. | Heating and cooling utilities; filters; spray parts; coating-solution losses; cleaning; maintenance; coating time; rework and yield loss. | Qualify utilities and controls; test airflow, spray delivery, alarms, and interlocks. Establish and verify operating ranges for process parameters, then assess coating performance and batch reproducibility. |
| Liquid preparation and mixing | Working volume; viscosity and mixing needs; temperature control; vessel pressure or vacuum rating; hygienic design; drainability; cleaning or sterilization approach. | Vessel and agitator specifications; material certificates; weld and surface-finish records where applicable; instrument details; cleaning-system compatibility; pressure-system documentation where relevant. | Vessel and agitator maintenance; seals and gaskets; heating or cooling; cleaning agents and water; calibration; downtime; product changeover and hold-time effects. | Review design and product-contact surfaces; verify installation and instruments; test mixing, temperature control, alarms, and drainability. Qualify cleaning or sterilization processes where required by the process and site procedures. |
| Filling and closing | Container and closure formats; fill-volume range; target throughput; product characteristics; line clearance; environmental controls; reject handling; inspection requirements. | Format and change-part documentation; fill-accuracy test method; controls and reject-system specifications; line integration plan; support for factory and site acceptance testing. | Format parts; seals and pumps; calibration; inspection equipment; changeover labor; consumables; line downtime; rejected units; maintenance and service. | Agree measurable acceptance criteria before factory acceptance testing (FAT) and site acceptance testing (SAT). Verify fill accuracy, reject challenges, alarms, line controls, and intended operating formats during OQ/PQ. |
| Cleaning, sterilization, and containment interfaces | Product and cleaning-agent compatibility; cleanability; equipment geometry; drainability; sterilization exposure where applicable; occupational exposure controls; facility and utility interfaces. | Cleaning and sterilization design information; material compatibility data; cycle or process records where applicable; containment performance basis; documented interface requirements. | Water, steam, energy, cleaning agents, filters, protective equipment, validation effort, maintenance, and production time lost to cleaning or turnaround. | Use a documented, risk-based approach. Establish cleaning acceptance criteria and verify the cleaning process; qualify sterilization cycles when required. Assess containment performance against the site-defined exposure-control strategy. |
| Supplier and service assessment | Required delivery date; installation scope; intended operating environment; training; service coverage; spare-parts availability; documentation language and format; change-control expectations. | Quality-system and documentation review; project references relevant to the equipment type; organization and escalation structure; service and parts commitments; cybersecurity and software lifecycle information when applicable. | Installation and commissioning; training; travel and service; spare-parts inventory; software support; upgrades; obsolescence; production impact during service events. | Define deliverables, responsibilities, and acceptance criteria in contracts and project plans. Maintain traceability from URS to design, testing, deviations, and release documentation. Apply risk-based computerized-system controls when software functions affect regulated records or decisions. |
| Total cost of ownership and final selection | Compare equivalent capacity, product-contact scope, automation, facility interfaces, and qualification deliverables. Document assumptions, production demand, and expected useful life. | Request itemized quotations and comparable scope; clarify exclusions, acceptance testing, warranty, service terms, spare parts, software licensing, and expected delivery milestones. | Model acquisition, installation, utilities, labor, consumables, maintenance, calibration, cleaning, validation, downtime, upgrades, and end-of-life costs over the planned evaluation period. | Score each option against approved requirements and quality risks. Select the option with justified process fit and supportability, not purchase price alone; approve a project-specific qualification plan before procurement or installation. |